Shanman (Linyi) Maquinaria Co., Ltd.

QT9-15 Máquina para fabricar ladrillos de hormigón

QT9-15 Máquina para fabricar ladrillos de hormigón

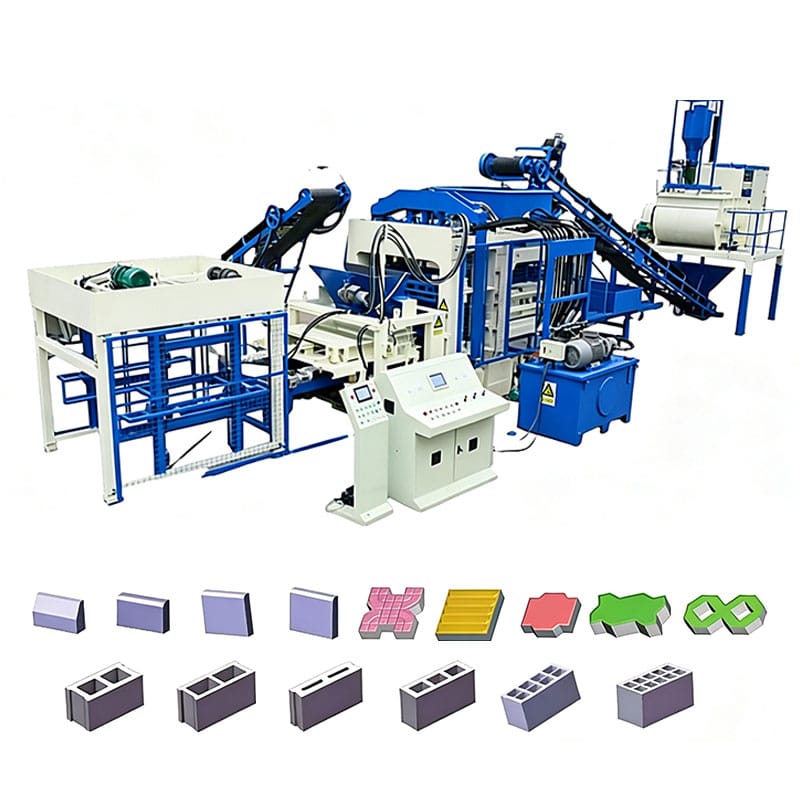
The QT9-15 concrete brick making machine is a large-scale, fully automatic block molding unit featuring an optimized design. Incorporating advanced German block-making technology, the machine is built for stability and heavy-duty performance.

Dimensiones: 3600 × 2300 × 2850 mm
Peso: 11 T
Ciclo de moldeo: 15-20 segundos

Overview

The QT9-15 concrete brick making machine is a large-scale, fully automatic block molding unit featuring an optimized design. Incorporating advanced German block-making technology, the machine is built for stability and heavy-duty performance.

Core Advantages

1. Four-Axis Synchronous Vibration System

Equipped with a Siemens control system and a four-axis synchronous vibration system, the machine offers stability and ease of operation. The energy-efficient vibration system allows for adjustable vibration intensity, minimizing damage to the equipment and molds. The variable-frequency synchronous vibration method delivers greater force, resulting in higher brick density and reduced cement consumption. With powerful excitation—featuring an amplitude of 2mm and acceleration of 15g—materials are rapidly molded in approximately two seconds.

2. Fully Automatic PLC Intelligent Control

The system utilizes computer control with an LCD touchscreen for parameter adjustment and includes data input/output interfaces for human-machine interaction. A built-in safety interlock prevents the execution of a subsequent action unless the preceding one has been correctly completed, thereby avoiding operational errors.

3. Efficient and Uniform Material Feeding System

Specialized rotary arch-breaking and horizontal grid feeding mechanisms allow for the selection of feeding methods tailored to specific products. The new semi-enclosed hopper and feeding cart—featuring gear-driven, 360-degree rotation—ensure rapid and uniform material distribution into the mold. The new feeding cart is also equipped with wear-resistant and leak-proof components.

4. Robust and Durable Machine Structure

Incorporating advanced German block-making technology, the machine features a heavy, stable structure—weighing 30% more than domestic models of similar output—which provides excellent vibration absorption. The frame utilizes thick-walled square tubing and extra-long guide sleeves to ensure structural rigidity, vibration resistance, and precise movement of the pressure head. With an ultra-low center of gravity and the vibrating table positioned just 486mm above the ground, 90% of residual vibration is transferred to the foundation, extending equipment lifespan. The guide columns are designed for permanent use without replacement, reducing maintenance costs.

5. Excellent Synchronization and Dimensional Precision

Adjustable synchronous swing arms are installed on both the pressure head and the demolding frame, ensuring that deviations in pressure head and demolding positioning remain within ±1mm. The pressure head employs a synchronous vibration-and-compression mechanism; its unique high-pressure design (capable of exerting up to 100 tons of force) guarantees high block strength and density. 6. Versatile Application & Flexible Mold Changing

By simply changing molds, the machine can produce a wide range of products, including hollow blocks, porous bricks, standard bricks, pavers, curbstones, grass pavers, washed-finish bricks, and more. With the addition of a secondary feeding system, multiple brick types can be produced simultaneously.

7. Wide Raw Material Adaptability

It utilizes industrial waste materials such as fly ash, furnace slag, metallurgical slag, steel slag, coal gangue, tailings sand, and construction waste, achieving a waste utilization rate of over 90%. By changing molds, the main production unit can manufacture porous bricks and hollow blocks in various specifications.

8. High Efficiency & Energy Saving

Incorporates German variable-frequency technology for superior energy efficiency and environmental friendliness, reducing power consumption by 30%. Uses a speed-increasing mechanism to optimize production speed and ensure efficient molding cycles. The synchronized gearbox is externally mounted to prevent oil leakage from the vibration box while simultaneously reducing vibration energy consumption.

Brick Types

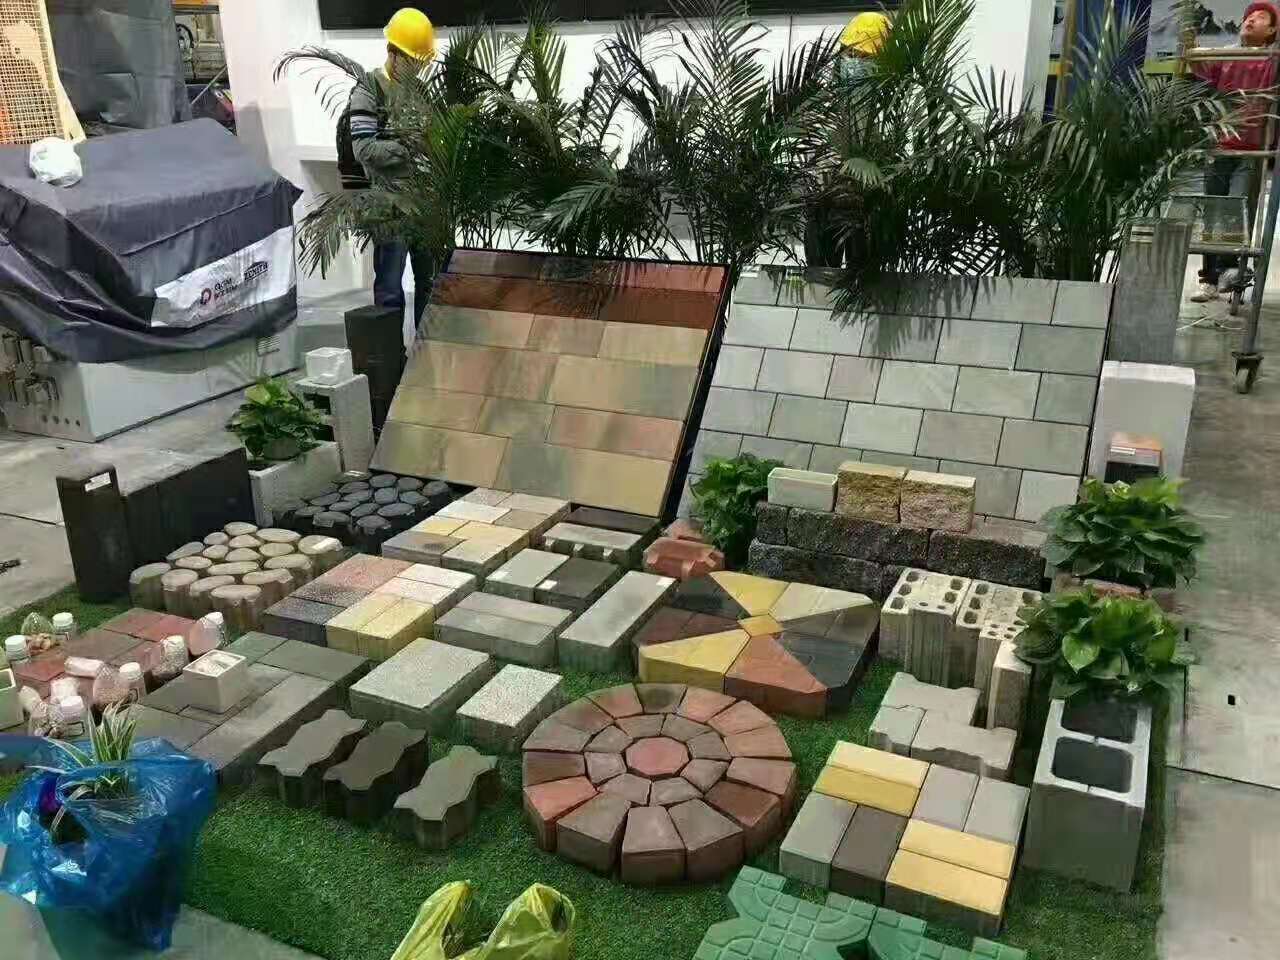
The QT9-15 brick-making machine allows for the flexible production of various brick types simply by changing molds:

• Hollow blocks: 390×190×190mm, 400×200×200mm, 400×150×200mm, etc.

• Porous bricks: 240×115×90mm, etc.

• Standard solid bricks: 240×115×53mm, etc.

• Pavers/Pavement bricks: 225×112.5×60mm, 200×100×60mm, etc.

• PC imitation-stone permeable bricks

• Interlocking blocks

• Curbstones/Embankment blocks

• Grass pavers, washed-finish bricks

• Composite thermal insulation concrete blocks

• Capable of producing colored pavers in various specifications with the addition of a color-facing material feeder

• Custom molds for special-shaped bricks available upon request
QT9-15 product detail

Real Customer Case Studies

Operation

Basic Working Principle

The core working principles of the QT9-15 brick making machine are as follows

1. Vertical directional vibration and pressure molding: Utilizes a multi-shaft rotary feeding device; forced centrifugal discharge is generated through the action of a swinging material distributor and an anti-arching mechanism.

2. Low-frequency feeding and high-frequency molding: Employs a fully synchronous vibration method; vibration force is adjustable, and frequency can be modified to meet specific process requirements.

3. Split-type coupled vibration: Doubles the effective vibration area and evenly distributes vibration force across all parts of the mold box, significantly enhancing product density and extending the service life of the mold box.

4. Rapid liquefaction and air release: Features powerful excitation force, an amplitude of 2mm, and an acceleration of 15g, enabling rapid material molding within approximately 2 seconds and ensuring full liquefaction of the cement.

5. Synchronous demolding: Demolding occurs synchronously after molding is complete, ensuring precise product dimensions and high density.

Workflow

The complete workflow of the QT9-15 fully automatic brick making machine is as follows

1. Batching: Automatic metering and batching are performed by a PL1600 three-bin batching station. Materials such as cement (from 50–100T silos) and fly ash are conveyed to the batching station via screw conveyors.

2. Mixing: Once batched, materials are transported by belt conveyor to a JS750 forced-action mixer for thorough mixing. 3. Material Feeding: The mixed material is conveyed into the block molding machine's main hopper by an 8-meter conveyor.

4. Material Distribution: The new semi-enclosed feeding hopper utilizes a gear drive and can rotate 360 ​​degrees, allowing for rapid and uniform material delivery into the mold. Specialized mechanisms—including a rotating arch-breaking distributor and a horizontal grid distributor—enable the selection of different feeding methods based on the specific product being manufactured.

5. Pressing and Molding: The press head employs synchronous vibration and compression; a unique high-pressure structure (capable of exerting up to 100 tons of force) ensures the blocks achieve high strength and density.

6. Synchronous Demolding: The bottom mold is equipped with a gear-rack synchronization system to ensure the blocks remain undamaged during the demolding process.

7. Block Discharge and Conveying: Finished blocks are discharged by a block-transfer mechanism and can be paired with a pallet elevator for automatic stacking.

Configuration

Equipment NameSpecifications
Cement Silo50–100T
Water ScaleWater for batching
Cement Scale300 kg
Screw Conveyor6.7 m
Three-Aggregate Batching StationPL1600 three-bin batching station for raw material proportioning
Belt Conveyor8 m conveyor for transporting mixed concrete to the main machine hopper
Forced MixerJS750 mixer for forced mixing of materials into uniform concrete
Mixed Material Conveyor8 m conveyor for transporting mixed concrete to the main machine hopper
Pallet FeederPallet conveyor feeding the brick-making machine
Block Molding MachineQT9-15
Brick Transfer/Stacking MachineAutomatic discharge and palletizing of finished bricks
Pallet ElevatorQT9-15 auxiliary equipment
Colored Brick System① Color mixer ② Color pigment conveyor ③ Color-dosing feeder

Optional equipment: loaders, forklifts, etc.

Specification

SpecificationsSpecification data
Machine dimensions3600x2300x2850
Machine weight11T
Molding cycle15-20 seconds
Vibration force (exciting force)80-105 KN
Vibration frequency2,800-45000 rpm
Control methodSiemens PLC fully automatic intelligent control, LCD touch screen, equipped with data input and output devices
Molding methodTable mold combined vibration + vertical directional vibration + pressure molding (pressure head pressure can reach 100T)
Number of operators6-10 people/shift
Voltage380V/220-440V (optional)
Compatible mixer modelJS750 mixer
Pallet dimensions1,400×720×30mm
Installation area requirementsAbout 300-400m²
Curing area for molded green bricksGenerally recommended 1000-3000m²
Water consumption for mixing8-15 tons/day
Water usage for natural curing of green bricksAbout 10-15 tons/day
Suitable raw materialsCement, gravel, sand, stone powder, fly ash, slag, slag, coal gangue, tailings sand, steel slag, ceramsite, perlite, construction waste, etc.

Capacity

The theoretical output of the QT9-15 brick-making machine varies by brick type, as follows

QT9-15 product detail
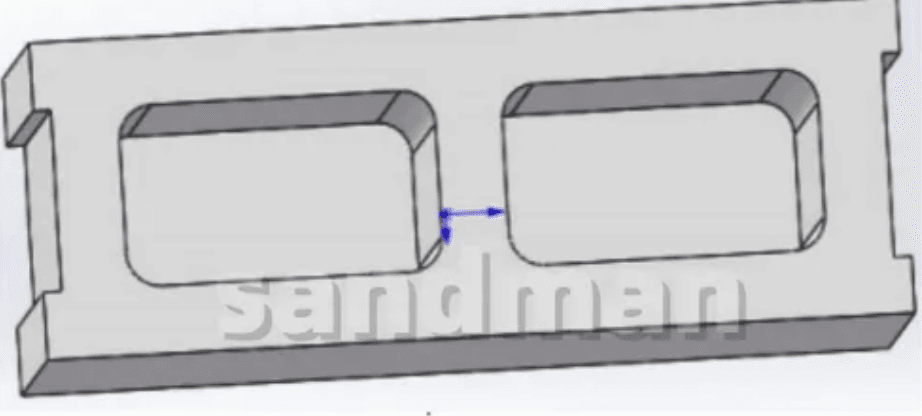
8”/400×200×200mm/2holes
Production Capacity
Per mold: 9 blocks – Per hour: Approx. 1620-2160 blocks – Per 8 hours: 11520-15360 blocks
QT9-15 product detail
6”/400×150×200mm/m/3holes
Production Capacity
– Per mold: 15 blocks -Per hour: Approx.2700-3600 blocks – Per 8 hours: 21600-28800blocks
QT9-15 product detail
4”/400×100×200mm/2holes
Production Capacity
-Per mold: 18 blocks -Per hour:Approx. 3240-4320blocks -Per 8 hours:25920-34560 blocks
QT9-15 product detail
200x100x60mm Rectangular Pavers
Production Capacity
– Per mold: 33 blocks – Per hour: Approx. 5940 blocks – Per 8 hours: 47520 blocks
QT9-15 product detail
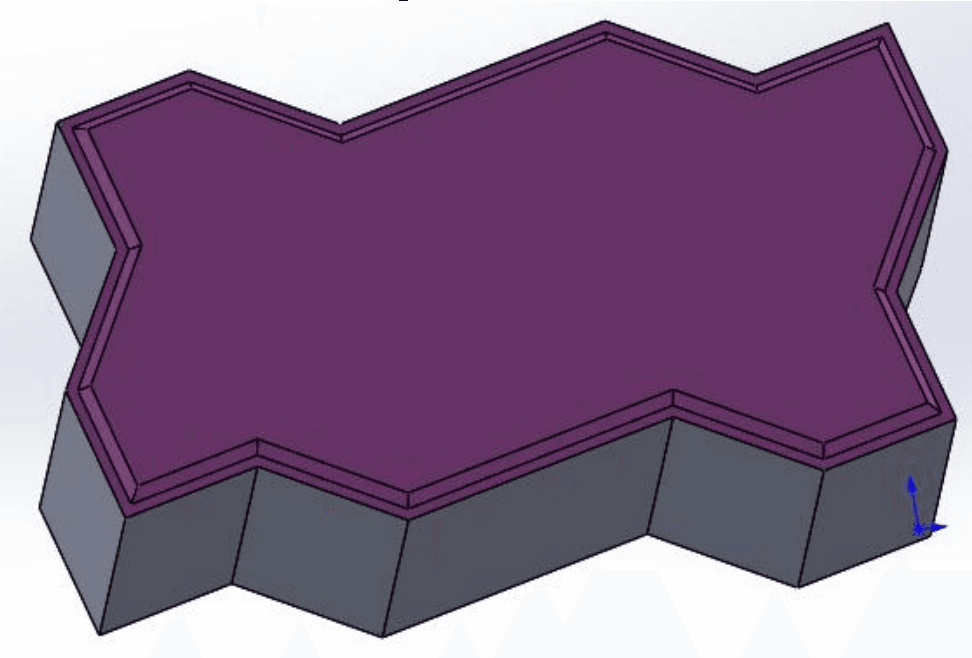
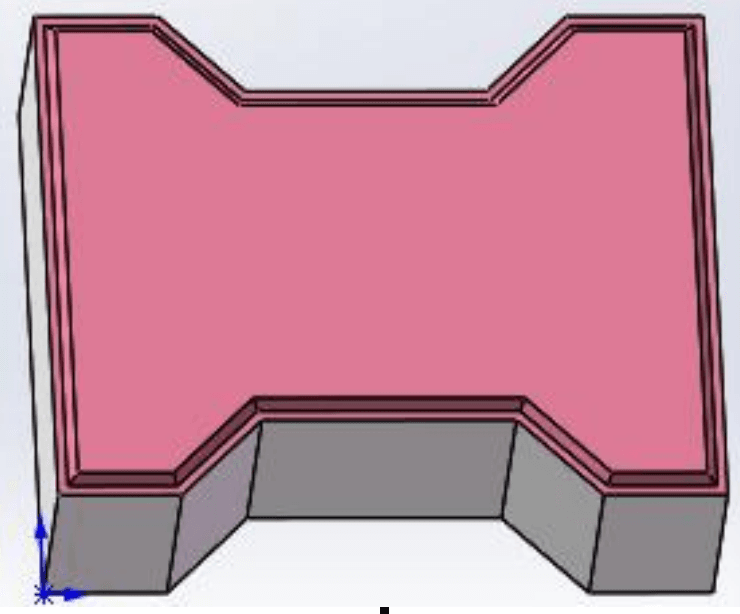
225×112.5x80mm
S-Shaped Pavers
Production Capacity
– Per mold: 25 blocks -Per hour: Approx. 4500-6000 blocks
-Per 8 hours: 36000-48000 blocks
QT9-15 product detail
200x163x60mm
I-Shaped Pavers
Production Capacity
Per mold: 21 blocks -Per hour: Approx. 3780 blocks – Per 8 hours: 30240 blocks

Note: The figures above represent theoretical maximums; actual output should be estimated at 85%–90% of the theoretical value (accounting for time spent on mold changes, cleaning, material feeding intervals, etc.).

Find the Right Brick Machine

Tell us your block type, target capacity, and budget. Our engineers will recommend the right production solution for your project.

OBTÉN COTIZACIÓN GRATIS

Demostración del formulario de contacto

By changing molds, the machine can produce hollow blocks, solid blocks, paving bricks, interlocking pavers, curbstones and other concrete products.

Common materials include cement, sand, crushed stone, fly ash, slag and other locally available aggregates. The exact mix depends on the required block strength and finish.

Yes. We can recommend or customize the machine configuration, mold design, production capacity and automation level according to your block samples and factory conditions.

Standard supply normally includes the main block machine, control system and selected mold. Mixers, conveyors, pallet systems and other auxiliary equipment can be added as required.

Yes. We provide installation guidance, commissioning, operator training, technical support and spare-parts service. Remote and on-site support options are available.

OBTÉN COTIZACIÓN GRATIS

Demostración del formulario de contacto