Шанман (Линьи) Машинери Ко, Лтд.

QT8-15 Машина для производства бетонного кирпича

QT8-15 Машина для производства бетонного кирпича

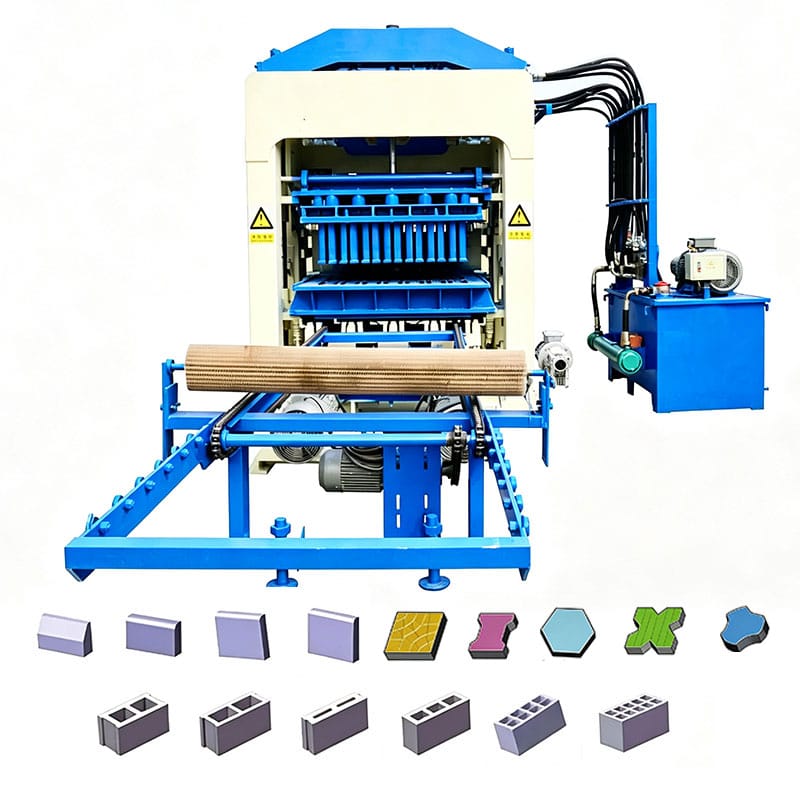
The QT8-15 concrete brick making machine is a fully automatic, multifunctional block molding system utilizing a combination of mechanical, hydraulic, and PLC control technologies. It represents a large-scale, fully automated production line characterized by high efficiency, stability, and intelligent operation.

Размеры: 3 800 × 2 200 × 2 750 мм
Вес: 10,5 Тл
Цикл формования: 15 — 20 секунд

Overview

The QT8-15 concrete brick making machine is a fully automatic, multifunctional block molding system utilizing a combination of mechanical, hydraulic, and PLC control technologies. It represents a large-scale, fully automated production line characterized by high efficiency, stability, and intelligent operation.

The QT8-15 features a PLC control system equipped with digital displacement sensing technology and a self-diagnostic system. It offers short molding cycles and high production efficiency, producing blocks with high density and precise dimensions.

Core Advantages

1. Fully Automatic PLC Intelligent Control

The control system effectively integrates digital and displacement sensing technologies, ensuring precise and reliable operation. An automated diagnostic system detects computer faults and issues alerts, facilitating timely troubleshooting.

2. High-Efficiency Multi-Source Vibration System

Designed for large-scale molding machines, this system integrates computer control, hydraulic drive, and electromechanical synchronization technologies. It employs a fully synchronous vibration method with adjustable impact force and frequency to meet diverse process requirements. Low-frequency feeding and high-frequency molding are utilized; excitation force is adjustable based on raw material characteristics to achieve optimal compaction, with vibration acceleration reaching up to 17.5G.

3. Uniform and Rapid Material Distribution System

A new semi-enclosed feed hopper, equipped with an internal linear reciprocating grid, ensures rapid and uniform material delivery into the mold. A uniquely designed material storage and distribution system guarantees feeding precision—supplying material exactly when needed with accurate volume—thereby ensuring consistent product density.

4. Robust and Durable Machine Structure

The machine frame is constructed from high-strength structural steel using specialized welding techniques, ensuring exceptional rigidity. Guide columns are made of ultra-strong special steel with a chrome-plated finish, offering superior torsional resistance and wear resistance. A four-rod guiding mechanism combined with extra-long guide bearings ensures precise movement of the pressure head and mold.

5. Versatile Application and Flexible Mold Changing

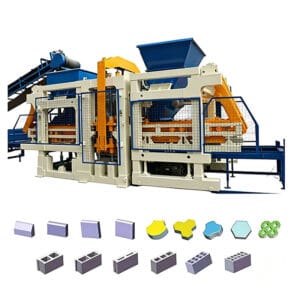
By simply changing molds, the machine can produce a wide range of concrete products, including hollow blocks, porous bricks, standard bricks, colored pavers, curbstones, grass pavers, and slope protection bricks.

6. Broad Raw Material Adaptability

The machine can utilize industrial by-products and waste materials—such as fly ash, slag, coal gangue, tailings, and construction debris—as raw materials, enabling the resource utilization of solid waste. VII. Brick Types Produced

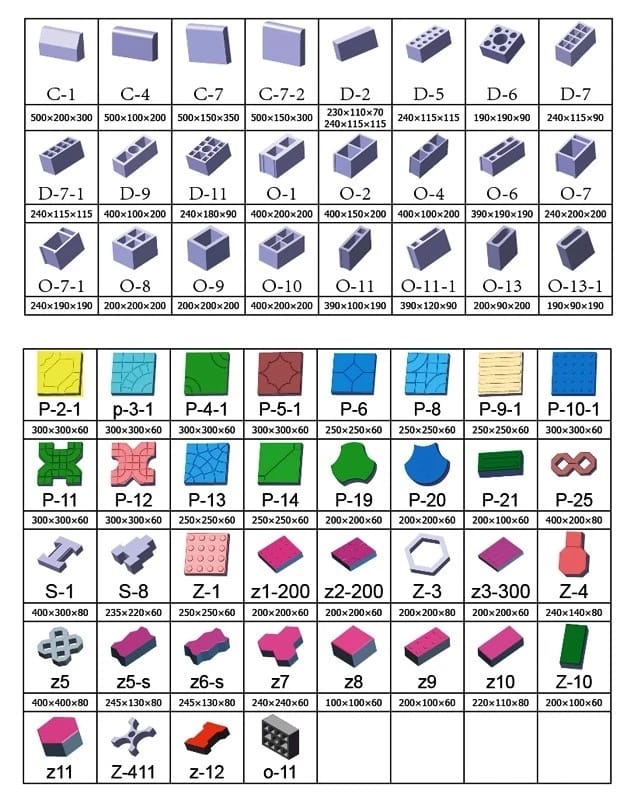
By simply changing molds, the QT8-15 brick-making machine can produce a wide variety of brick types

• Hollow blocks: 390×190×190mm, 400×200×200mm, etc.

• Multi-hole bricks: 240×115×90mm, 240×180×90mm, etc.

• Standard solid bricks: 240×115×53mm, etc.

• Pavers/paving bricks: 200×100×60mm, 200×163×60mm, 225×112.5×60mm, etc.

• Interlocking blocks, curbstones

• Grass pavers, slope protection bricks

• Capable of producing colored pavers and similar products when equipped with a face-mix device

• Molds for special-shaped bricks can be customized according to user requirements
QT8-15 product detail

Real Customer Case Studies

Operation

Basic Working Principle

The core operating principles of the QT8-15 brick making machine are as follows

1. Mechanical-Hydraulic Synergy: Employs a molding method combining hydraulic and mechanical systems, utilizing both vibration and compression to form the blocks.

2. Vertical Directional Vibration & Compression: Uses vertical directional vibration and compression within the mold box; a multi-axis rotary feeding device works in tandem with an arch-breaking rake to distribute material evenly.

3. Low-Frequency Feeding & High-Frequency Molding: Utilizes fully synchronous vibration. The impact force and frequency are adjustable to meet specific process requirements (low frequency for feeding, high frequency for molding). Excitation force is adjusted based on raw materials to achieve optimal compaction, with vibration acceleration reaching up to 17.5G.

4. Rapid Air Evacuation: Hydraulic-driven vertical synchronous vibration (with adjustable frequency and amplitude) is controlled by the computer, allowing the concrete to fully evacuate air and densify within a short period.

5. Synchronous Demolding: Demolding occurs synchronously after the molding process is complete, ensuring precise product dimensions and high density.

The finished blocks achieve a compressive strength of up to 15 MPa and high density, offering superior water and frost resistance, as well as excellent sound insulation and thermal insulation properties.

Workflow

The complete workflow of the QT8-15 fully automatic brick making machine is as follows

1. Batching: A loader transfers raw materials (such as waste residue) into the hopper of the PL1200 batching machine, while materials like cement or fly ash are conveyed to the hopper via a screw conveyor; batching and metering are performed according to formulas stored in the computer system. 2. Mixing: Once proportioned, the materials are transported via conveyor belt to the JS750 mixer for blending.

3. Material Feeding: The mixed material is conveyed into the large hopper of the block molding machine.

4. Material Distribution: The new semi-enclosed feed hopper features a linear reciprocating mesh screen to rapidly and evenly deposit material into the mold. Utilizing sensor technology and proportional hydraulic drives, the system employs an oscillating distribution carriage and an anti-arching mechanism to achieve forced centrifugal discharge, ensuring rapid and uniform material distribution.

5. Pressing and Molding: The press head descends while the table mold vibrates; a computer-controlled, hydraulically driven multi-source vibration system generates synchronized vertical vibration.

6. Synchronized Demolding: Demolding occurs simultaneously upon completion of the molding process.

7. Block Discharge and Conveying: Finished blocks are discharged by the block delivery unit and can be automatically stacked using a palletizer.

Configuration

Equipment NameSpecifications
Automatic Batching SystemSN100 cement silo, electronic cement scale, screw conveyor, PL1200 batching machine, and belt distributor; features computer-based automatic control technology, automatic calibration, and automatic drop correction for precise measurement.
Mixing SystemJS750 forced-action mixer and 8m belt conveyor; mixes materials according to the preset ratio and delivers them to the molding machine's main hopper.
Molding SystemQT8-15 block molding machine, pallet feeder, brick unloader, hydraulic system, and automatic control system; a face-mix feeder is required for producing colored products.
Brick StackerAutomatic palletizing of finished bricks.
Manual Pallet Truck / Green Brick Transfer CartTransfer of finished green bricks.
MoldCustomized according to the required brick type.

Specification

SpecificationsSpecifications
Main machine dimensions3,800 × 2,200 × 2,750 mm
Main machine weight10.5 t
Molding cycle15–20 seconds
Vibration force (exciting force)70–100 kN
Vibration frequency2,800–4,500 cycles/min (50–90 Hz)
Main machine power (installed capacity)45 kW
Control methodFully automatic intelligent PLC control with fault self-diagnosis system
Molding methodCombined table/mold vibration + vertical directional vibration + pressure molding
Number of operators5–8 persons/shift
Voltage380 V / 220–440 V (customizable)
Compatible mixer modelJS750 mixer
Pallet dimensions1,050 × 900 × 28 mm
Installation area requirementsApprox. 250–300 m²
Curing area for molded green bricks1,000–2,000 m²
Water consumption for mixingApprox. 6–10 tons/day
Water usage for natural curing of green bricksApprox. 8–12 tons/day (depending on climate and output)
Suitable raw materialsCement, crushed stone, sand, stone dust, slag, fly ash, coal gangue, tailings, construction waste, etc.

Capacity

QT8-15 product detail
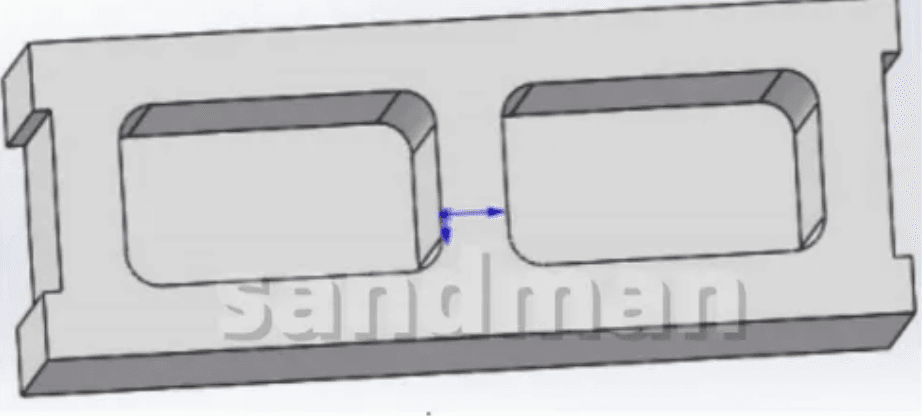
8”/400×200×200mm/2holes
Production Capacity
Per mold: 8 blocks – Per hour: Approx. 1440-1920 blocks – Per 8 hours: 11520-15360 blocks
QT8-15 product detail
6”/400×150×200mm/m/3holes
Production Capacity
– Per mold: 12 blocks -Per hour: Approx.2160-2880 blocks – Per 8 hours: 17280-23040 blocks
QT8-15 product detail
4”/400×100×200mm/2holes
Production Capacity
-Per mold: 16 blocks -Per hour:Approx. 2880-3840 blocks -Per 8 hours: 23040-30720blocks
QT8-15 product detail
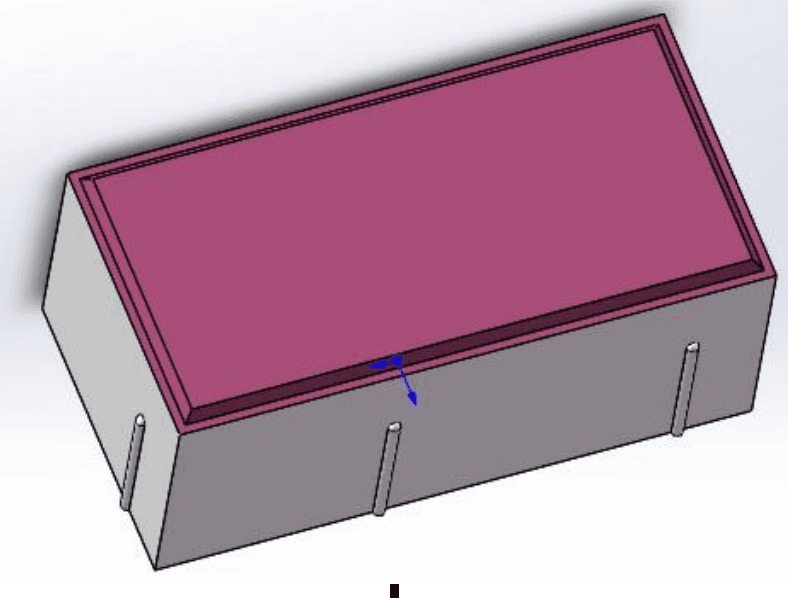
200x100x60mm Rectangular Pavers
Production Capacity
– Per mold: 28 blocks – Per hour: Approx. 5040 blocks – Per 8 hours: 40320blocks
QT8-15 product detail
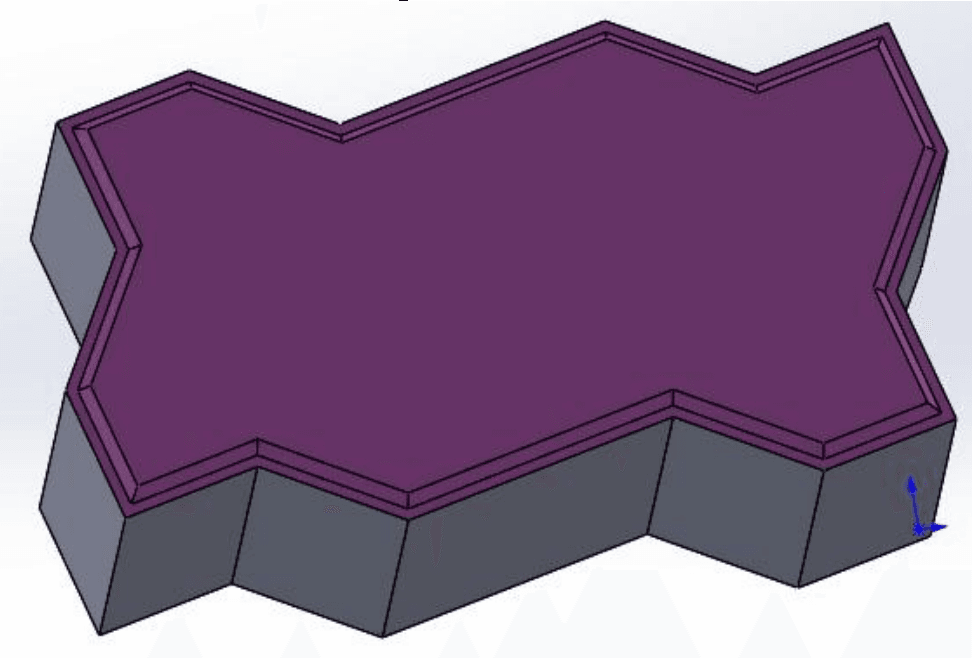
225×112.5x75mm
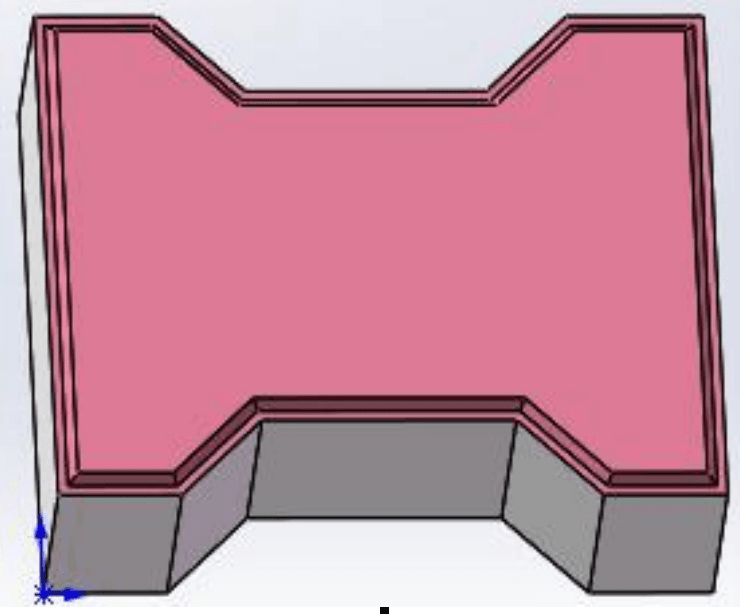
S-Shaped Pavers
Production Capacity
– Per mold: 24 blocks -Per hour: Approx. 4320 blocks
-Per 8 hours: 34560 blocks
QT8-15 product detail
200x163x60mm
I-Shaped Pavers
Production Capacity
Per mold: 20 blocks -Per hour: Approx. 3600 blocks – Per 8 hours: 28800 blocks

All output figures represent actual, continuous production capacity—no inflated or exaggerated claims.

Want to know more about production rates for different brick types? Contact us today.

ПОЛУЧИТЬ БЕСПЛАТНУЮ ЦИТАТУ

Контактная форма Демо

By changing molds, the machine can produce hollow blocks, solid blocks, paving bricks, interlocking pavers, curbstones and other concrete products.

Common materials include cement, sand, crushed stone, fly ash, slag and other locally available aggregates. The exact mix depends on the required block strength and finish.

Yes. We can recommend or customize the machine configuration, mold design, production capacity and automation level according to your block samples and factory conditions.

Standard supply normally includes the main block machine, control system and selected mold. Mixers, conveyors, pallet systems and other auxiliary equipment can be added as required.

Yes. We provide installation guidance, commissioning, operator training, technical support and spare-parts service. Remote and on-site support options are available.

ПОЛУЧИТЬ БЕСПЛАТНУЮ ЦИТАТУ

Контактная форма Демо